



B21, China Town Mall, Midrand
 Building Boards & Insulation
 Coated & Treated Products
Decorative Building Materials
EPDM/PVC/TPO Membrane
 Flat Products (Sheets, Plates & Coils)
Gabion mesh
Geocell
Geogrid
Geomembrane Welding machine
HDPE Geomembrane
HDPE Geomembrane
Hdpe/Pvc Pipe
Industrial Hardware & Fasteners
LDPE LLDPE Geomembrane
Luxury Wall Panels
Nonwoven Geotextile
Other Geosynthetics
Pipe Floater
Pipeline & Fluid Systems
Pipes & Hollow Sections
PVC Ceilings
PVC Cornices
PVC Suspended Ceilings
PVC Wall Panels
Roofing & Cladding
Roofing & Corrugated Sheets
Rubber Hose
SPC Flooring
Strips & Bars
Structural Steel & Profiles
 Camera & Photo
 Chargers, Batteries & Power Supplies
 Commercial Equipment
 Home Audio & Video
 Portable Audio
 Printing Equipment
 Professional Audio
 Security & Protection
 Testing Equipment
 Advertising Boards
 Advertising Inflatables
 Advertising Light Boxes
 Commercial Fryers
 Computer Hardware & Software
 Digital Signage and Displays
 Display Racks
 Food Trucks
 Ice Cream Machines
 Interactive Boards
 Photo Booths
 Projectors & Presentation Equipments
 Refrigeration Equipment
 Supermarket Shelves
 Vending Machines
 Bedroom Furniture
 Commercial Furniture
 Decorations
 Dining Room Furniture
 Kitchen Furniture
 Living Room Furniture
 Office Furniture
 Agriculture Machinery
 Apparel Machinery
 Chemical Machinery
 Cleaning Equipment
 Construction Machinery
 Environmental Machinery
 Food & Beverage Machinery
 Industrial Machinery
 Machine Tool Equipment
 Machinery Accessories
 Material Handling
 Packaging Machines
 Brick Making Machinery
 Concrete Mixers
 Concrete Pumps
 Crushers
 Drilling Rigs
 Engineering & Construction Machinery
 Excavators
 Gas Generation Equipment
 Loaders
 Mineral Separators
 Mining Machinery
 Mortar Spray Machines
 Other Construction Machinery
 Road Machinery
 Stone Machinery
 Tile Making Machinery
 Truck Cranes
 Baking Equipments
 Beverage & Wine Machines
 Cake machine
 Donut machines
 Fermenting Equipment
 Fish Processing Machines
 Flour & Rice Mills
 Flour Mill
 Food Sterilizers
 Fruit & Vegetable Processing Machines
 Fruit & Vegetable Processing Machines
 Fryers
 Ice Cream Machines
 Juice Extractors
 Meat Processing Machinery
 Meat Slicers
 Other Food Processing Machinery
 Popcorn machine
 Snack Machines
 Vegetable Cutters
 Vegetable Washing Equipments
 Apparel & Textile Machinery
 CNC industrial Machinery
 Industrial Compressors & Parts
 Industrial Robots
 Industry Laser Equipment
 Machine Tool Equipment
 Manufacturing Machinery
 Metal & Metallurgy Machinery
 Paper Production Machinery
 Plastic & Rubber Processing Machinery
 Welding Equipment
 Woodworking Machinery
 Animal & Veterinary
 Household Medical Devices
 Medical Consumables
 Professional Medical Devices
 Testing Instrument
 Bone Surgical Instruments
 Burns Surgery Instruments
 Clinical Analytical Instruments
 Clinics Apparatuses
 Dental Chair
 Dental Consumables
 Dental Equipments
 Dental Handpiece
 Diagnostic Apparatuses
 Emergency & Clinics Apparatuses
 General Assay & Diagnostic Apparatuses
 Hospital Beds
 Hospital Chairs
 Hospital Trolley
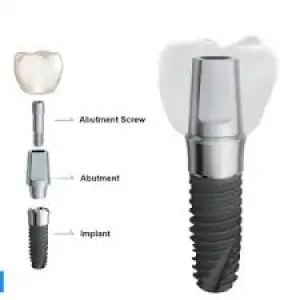 Implants & Interventional Materials
 Medical Cryogenic Equipments
 Medical Imaging Equipment
 Medical Optical Instruments
 Medical Ultrasound Instruments
 Medical X-ray Equipments
 Obstetrics & Gynecology Equipments
 Oral Therapy Equipments
 Physical Therapy Equipment
 Radiology Equipment & Accessories
 Rehabilitation Equipment
 Stethoscope
 Surgical Instruments
 Transfusion, Dialysis & Circulation Machines
 Vacuum Suction Devices
 Visual Acuity Examination Supplies
 Featured Accessories
 Mobile Phones
 Phone Accessories
 Screen Protector Machines
 Tablets
 Telecommunications
 Broadcast Intercom Systems
 Camera Modules
 Communication Antennas
 Corded Telephones
 Development Boards, Kits
 Enterprise Firewalls
 Enterprise Switches
 Fiber Optic Equipment
 Fixed Wireless Terminals
 Other Telecommunications Products
 PBX
 Signal conversion Boards
 Telecom Parts
 Wireless Infrastructure Equipment

Select a product option to continue.
Explore funding with Afrimart's partners. Subject to provider approval.

Detailed equipment flow description

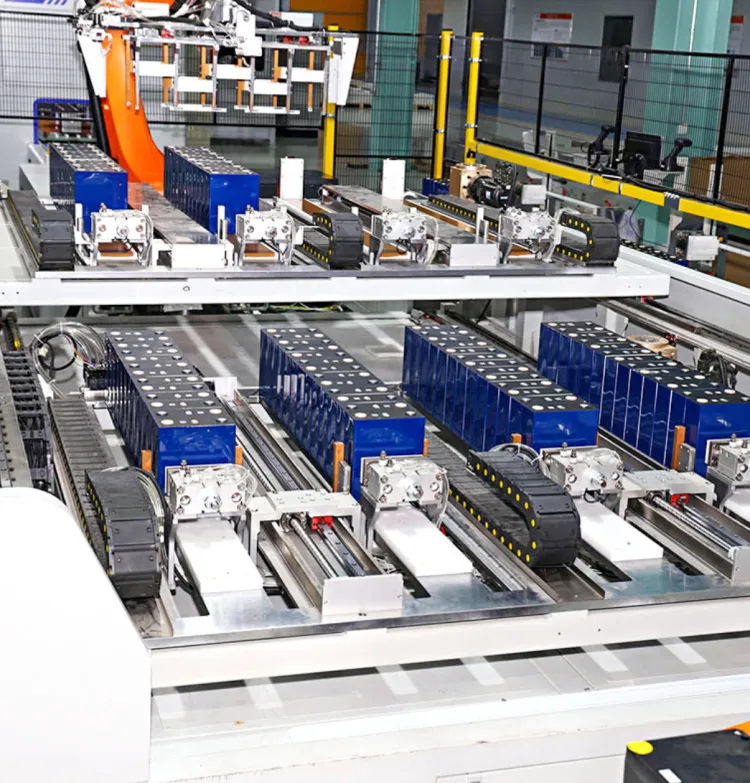
Cell section introduction

Parameter introduction:
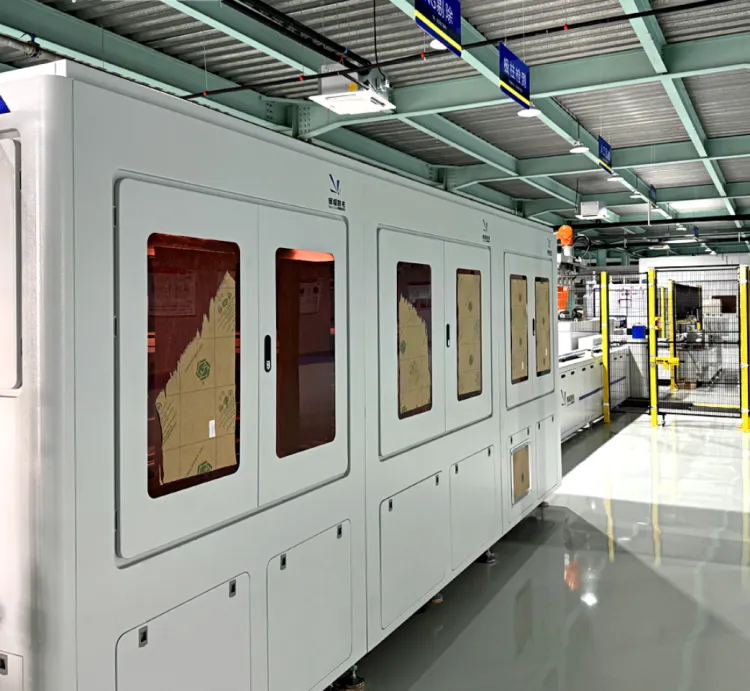
1. The total size of the cell section (L*W*H) is: 15m*4.6m*2.5m high; 2. The main functions of the battery cell section equipment: after the battery cell is online, the battery cell is sorted, the outer surface of the battery cell is cleaned by plasma, the battery cell is glued, the battery cell is stacked, and the module is offline and stand still.
Functional module design description-sorting/cleaning station

Function Description:
1. The equipment mainly realizes the functions of cell sorting and cell cleaning; 2. Work flow: After the cells are online, the cells are sorted, and the qualified cells are flowed into the next station. The unqualified cells are automatically picked out by the NG material mechanism to the unqualified assembly line; the qualified cells enter the cleaning station and automatically conduct electricity. Plasma cleaning of the core surface automatically flows into the next station after cleaning; automatic operation from loading to unloading, and the operation of the equipment and status feedback are controlled by the console.
Functional module design description-glue application station

Function Description:
1. This equipment mainly realizes the function of cell gluing; 2. Work flow: The operator puts the battery into the gluing position of the dispenser after taking the battery at the battery take-out position. The three-axis gluing mechanism drives the gluing head to apply the glue according to the set gluing track. After the gluing is completed, the glue is applied Manually take it out and put it on the buffer line; the glue applicator is divided into left and right double stations to run. 3. The station is a dual-line parallel station, composed of two dispensers, which can operate on a single line alone or on two lines at the same time.
Functional module design description-stacking extrusion station

Function Description:
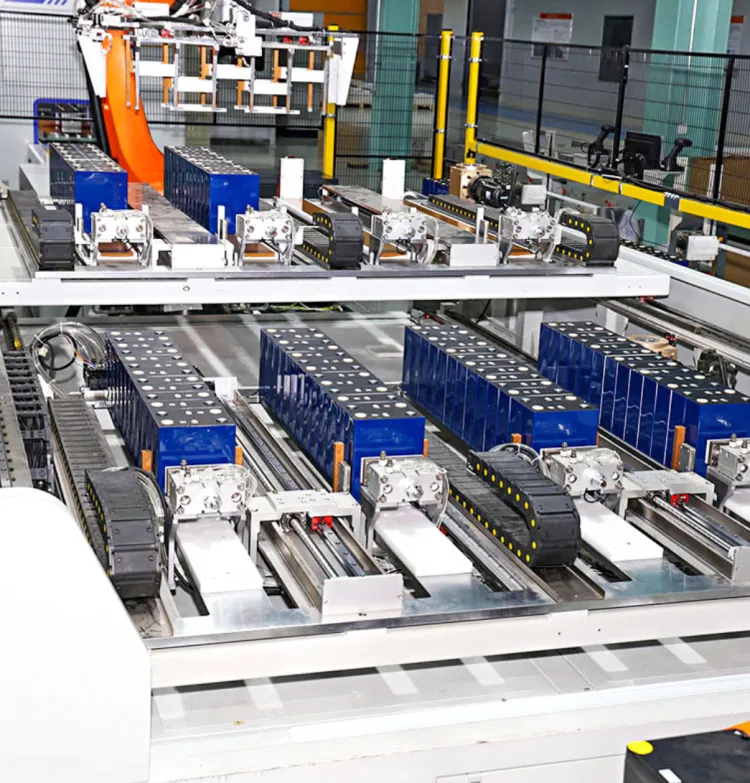
1. This equipment mainly realizes battery cell stacking, extrusion, bundling and packaging; 2. Work flow: After the glue-coated batteries are placed in the upper material position in turn, manually push into the extrusion position, start the extrusion mechanism button to make the batteries squeeze to the set pressure, put them into the strapping steel band, and then squeeze The pressing mechanism is retracted, and the squeezed module is manually retracted to the loading position. The cantilever crane and the stationary bottom plate are hoisted into the stationary trolley and pushed to the stationary area to stand still. 3. The station is divided into left and right stations, which can realize interchangeable double station operation such as station 1 extrusion and station 2 loading.
Functional module design description-module scan code/cleaning station

Function Description:
1. This equipment mainly realizes the module scan code binding and pole photo cleaning after the module goes online; 2. Work flow: The finished module is hoisted from the gantry crane to the loading position of the module. The module flows into the scan code binding position with the pallet. After lifting and positioning, manually hold the scan gun to the cell QR code and end plate The QR code is scanned sequentially. After the entry is completed, it flows into the pole cleaning position. After the position is visually photographed and checked, the pole cleaning is performed. After the cleaning is completed, it flows into the next station.
Functional module design description—module welding station

Function Description:
1. This equipment mainly realizes module pole welding; 2. Work flow: After the module has placed the adapter sheet, it flows into the station. After the jacking and positioning, the visual photograph is taken and the distance measurement record data is sent to the control system for welding position compensation. After the data is completed, the welding is automatically started, and the welding is completed. The positioning is opened, and the module flows into the next station with the tray.
Functional module design description—EOL inspection station

Function Description:
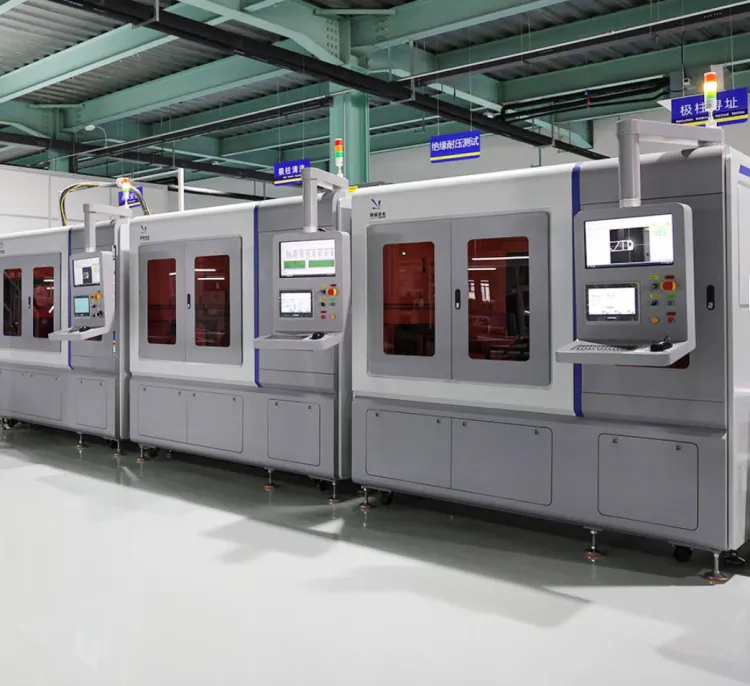
1. This equipment mainly realizes module performance testing after module welding, and is a manual auxiliary station; 2. Work flow: After the module is welded, it flows into the station. After the jacking mechanism is positioned, the operator connects the test plug with the module interface, and then activates the detection button. After the test is completed, the operator removes the connector and flows into the next job. Bit
Functional module design description-tray introduction

Function Description:
1. This component is located on the circulating tray on the welding assembly line, and the battery cell module is loaded for circulation on the double-speed chain; 2. Work flow: After putting the battery core into the tray, the locking mechanism locks the battery core.
Functional module design description-introduction to the trolley

Function Description:
This part is the operating tooling, which mainly transfers the extrusion module to stand still, and the module is welded on-line and off-line for transfer.
Layout introduction

Parameter introduction:
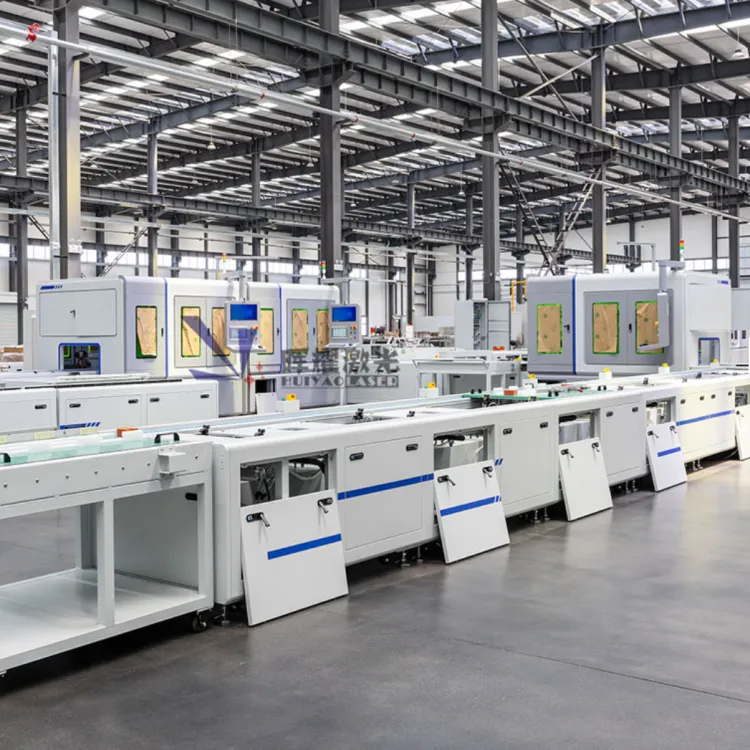
1. Layout plant size (L*W*H): 35m*9m*3m (may change with the refinement of the plan, the picture is for reference only) 2. Main functions: The design of the production line is divided into cell section and module section; the function of cell section is to process the sorting of cells after going online, cell surface cleaning, cell gluing, cell stacking; module section The functions include scanning code binding, pole cleaning, module welding, and post-welding EOL detection after the module is online.
Design requirements
1. Compatible with a variety of sizes of module specifications, quick type change;2. Realize intelligent chemical station and reduce the labor load of personnel;3. The battery cell section is flexibly associated with the module welding section and can be operated independently;4. The cell section is equipped with cell sorting, plasma cleaning, cell gluing, cell stacking, etc.;5. The welding section has the functions of loading module scan code binding, pole cleaning (photograph), laser welding, post-welding EOL detection, etc.;6. Equipment noise ≤75 (measured at 1000mm away from the operating position or the outer wall of the equipment);
Specification
| XYZ Travel | Customizable |
| R Axis | Optional, 360° rotation |
| Position Accuracy | ±0.02mm |
| Repeatability Accuracy | ±0.01mm |
| Motion Source | Step motor or Servo motor |
| Max Speed | 500mm/s |
| Cooling Method | Water cooling |
| Electricity Demand | Customizable |
| Laser Wavelength | 1080nm |
| Gas Protection | Optional, Argon, Nitrogen |
| Environmental Requirements | No vibration, interference and ventilation |
| Welding Penetration | 0.1~3.0mm |
| XYZ Travel | Customizable |
|---|---|
| R Axis | Optional, 360° rotation |
| Position Accuracy | ±0.02mm |
| Repeatability Accuracy | ±0.01mm |
| Motion Source | Step motor or Servo motor |
| Max Speed | 500mm/s |
| Cooling Method | Water cooling |
| Electricity Demand | Customizable |
| Laser Wavelength | 1080nm |
| Gas Protection | Optional, Argon, Nitrogen |
| Environmental Requirements | No vibration, interference and ventilation |
| Welding Penetration | 0.1~3.0mm |
| 1. The total size of the cell section (L*W*H) is | 15m*4.6m*2.5m high; 2. The main functions of the battery cell section equipment: after the battery cell is online, the battery cell is sorted, the outer surface of the battery cell is cleaned by plasma, the battery cell is glued, the battery cell is stacked, and the module is offline and stand still. |
| 1. The equipment mainly realizes the functions of cell sorting and cell cleaning; 2. Work flow | After the cells are online, the cells are sorted, and the qualified cells are flowed into the next station. The unqualified cells are automatically picked out by the NG material mechanism to the unqualified assembly line; the qualified cells enter the cleaning station and automatically conduct electricity. Plasma cleaning of the core surface automatically flows into the next station after cleaning; automatic operation from loading to unloading, and the operation of the equipment and status feedback are controlled by the console. |
| 1. This equipment mainly realizes the function of cell gluing; 2. Work flow | The operator puts the battery into the gluing position of the dispenser after taking the battery at the battery take-out position. The three-axis gluing mechanism drives the gluing head to apply the glue according to the set gluing track. After the gluing is completed, the glue is applied Manually take it out and put it on the buffer line; the glue applicator is divided into left and right double stations to run. 3. The station is a dual-line parallel station, composed of two dispensers, which can operate on a single line alone or on two lines at the same time. |
| 1. This equipment mainly realizes battery cell stacking, extrusion, bundling and packaging; 2. Work flow | After the glue-coated batteries are placed in the upper material position in turn, manually push into the extrusion position, start the extrusion mechanism button to make the batteries squeeze to the set pressure, put them into the strapping steel band, and then squeeze The pressing mechanism is retracted, and the squeezed module is manually retracted to the loading position. The cantilever crane and the stationary bottom plate are hoisted into the stationary trolley and pushed to the stationary area to stand still. 3. The station is divided into left and right stations, which can realize interchangeable double station operation such as station 1 extrusion and station 2 loading. |
| 1. This equipment mainly realizes the module scan code binding and pole photo cleaning after the module goes online; 2. Work flow | The finished module is hoisted from the gantry crane to the loading position of the module. The module flows into the scan code binding position with the pallet. After lifting and positioning, manually hold the scan gun to the cell QR code and end plate The QR code is scanned sequentially. After the entry is completed, it flows into the pole cleaning position. After the position is visually photographed and checked, the pole cleaning is performed. After the cleaning is completed, it flows into the next station. |
| 1. This equipment mainly realizes module pole welding; 2. Work flow | After the module has placed the adapter sheet, it flows into the station. After the jacking and positioning, the visual photograph is taken and the distance measurement record data is sent to the control system for welding position compensation. After the data is completed, the welding is automatically started, and the welding is completed. The positioning is opened, and the module flows into the next station with the tray. |
| 1. This equipment mainly realizes module performance testing after module welding, and is a manual auxiliary station; 2. Work flow | After the module is welded, it flows into the station. After the jacking mechanism is positioned, the operator connects the test plug with the module interface, and then activates the detection button. After the test is completed, the operator removes the connector and flows into the next job. Bit |
| 1. Layout plant size (L*W*H) | 35m*9m*3m (may change with the refinement of the plan, the picture is for reference only) 2. Main functions: The design of the production line is divided into cell section and module section; the function of cell section is to process the sorting of cells after going online, cell surface cleaning, cell gluing, cell stacking; module section The functions include scanning code binding, pole cleaning, module welding, and post-welding EOL detection after the module is online. |
The main functions include cell sorting, plasma cleaning, cell gluing, stacking, module scanning, welding, and post-welding inspection.
The total size of the cell section is 15m in length, 4.6m in width, and 2.5m in height.
Yes, the cell section and module welding section can operate flexibly and independently.
The maximum speed of the machine is 500mm/s.
The production line can use either step motors or servo motors, depending on customization.
The cleaning is performed using a plasma cleaning process to clean the outer surface of the battery cell.
The environment should have no vibration, interference, and proper ventilation for optimal operation.
Yes, the machine specifications such as electricity demand and XYZ travel can be customized.
Quality control is ensured through automatic sorting of qualified cells and EOL (End of Line) inspections after module welding.
The equipment noise level is ≤75 dB when measured at 1000mm away from the operating position or outer wall.
Optional gas protection can include Argon or Nitrogen.
The production line is designed to be compatible with a variety of sizes of module specifications.
The tray is used for circulating the battery cell modules, while the trolley transfers the extrusion modules to the next stations.
A three-axis gluing mechanism drives the gluing head to apply glue according to a set gluing track.
The repeatability accuracy of the machine is ±0.01mm.
Discover our latest orders